Custar Stone Enhances Plant Performance with Advanced Material Processing Solutions
Case Studies
Custar Stone Company, located in Custar, Ohio, has long been recognized as a trusted producer of high-quality limestone products serving the Northwest Ohio region. As a division of The Gerken Companies, Custar Stone plays an essential role in supplying construction-grade aggregates used in road building, infrastructure development, and a wide variety of commercial and municipal projects. With decades of experience and a strong reputation for reliability, the company has remained committed to maintaining efficient operations while meeting the evolving demands of the construction industry.
Challenge
In 2025, Custar Stone faced a critical turning point in its operations. The company began evaluating the need to replace its aging aggregate processing plant with newer, safer and more efficient equipment that could better support long-term production goals.
“The mill that we were using upstairs was built in 1953,” said Kevin Maassel, Superintendent Supervisor at Custar Stone. “It had lived its life and purpose, and we started this new plant operation late fall of 2025.”
The outdated mill had not only reached the end of its functional lifespan, but it also posed limitations in terms of efficiency, maintenance costs and operational safety. Continuing to rely on aging infrastructure would have risked production slowdowns and increased downtime, negatively impacting both output and profitability.
Custar Stone needed a solution that would allow them to maintain ongoing operations while simultaneously constructing a new facility. The existing mill, located on an upper bench, had to remain operational until sufficient space on the lower portion of the site was prepared to accommodate the new plant layout.
Solution
Custar Stone turned to McLanahan, a familiar and trusted partner, to address this challenge. The company had previously worked with McLanahan when replacing a smaller, outdated screw washer in the original processing plant. That positive experience gave them confidence in both the equipment and the support provided.
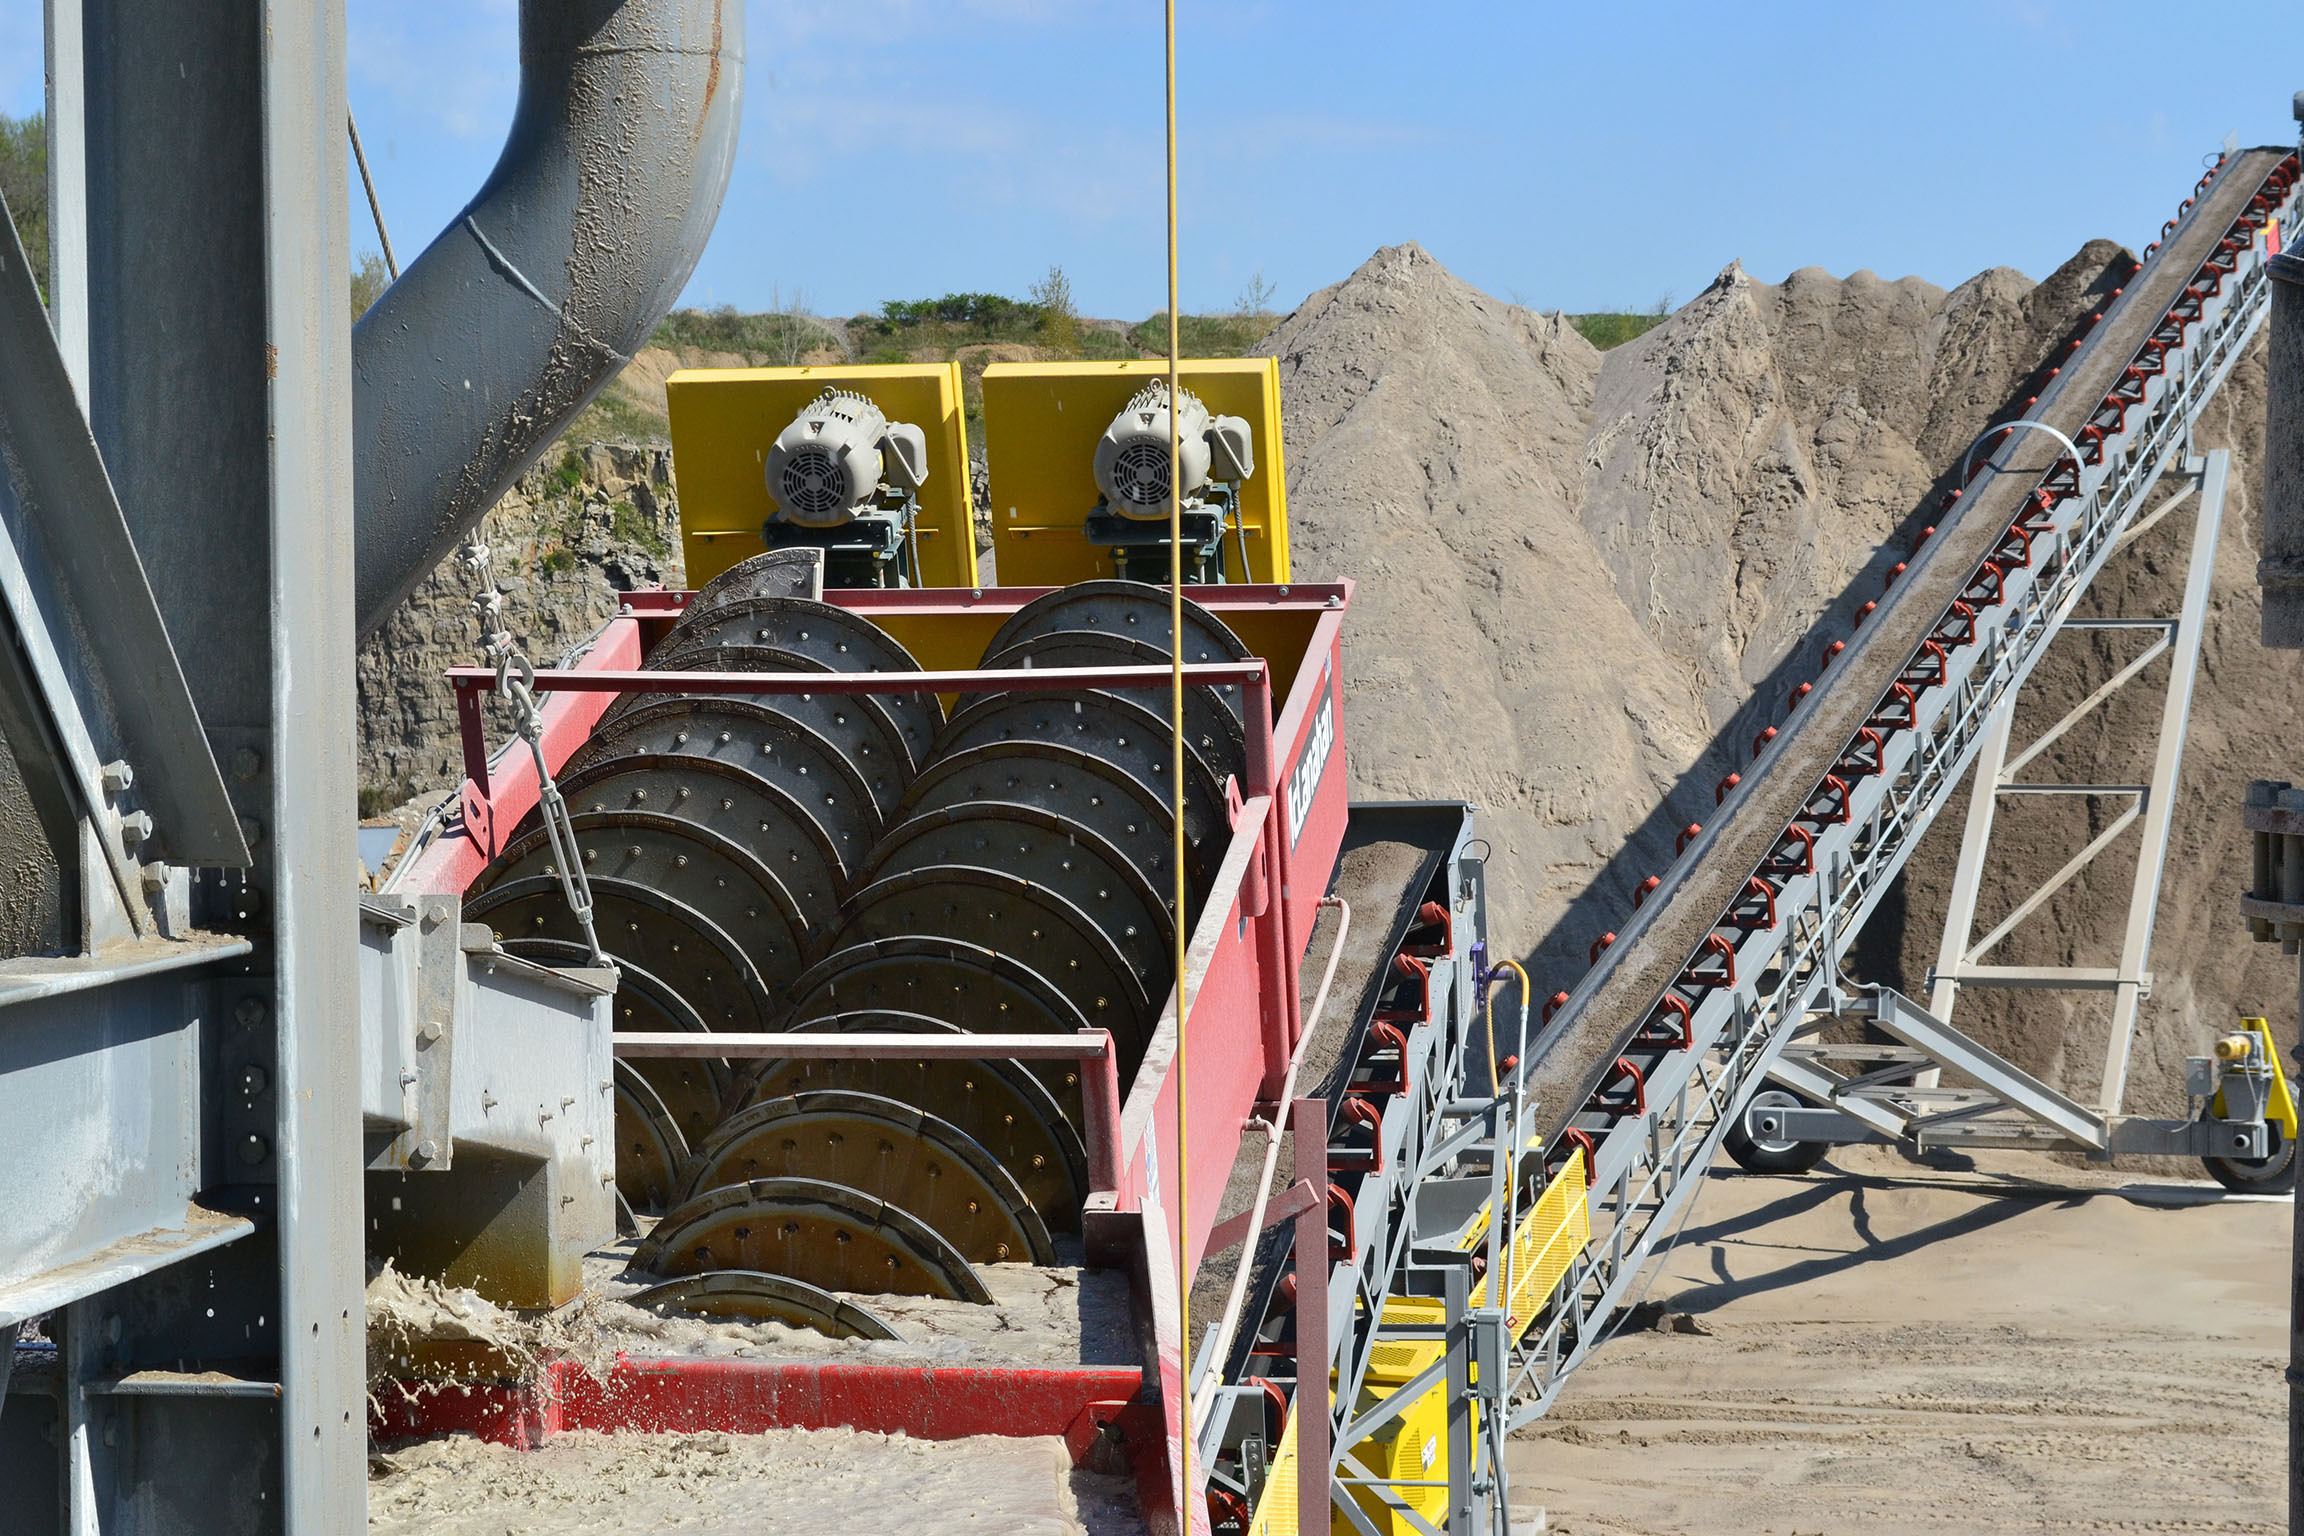
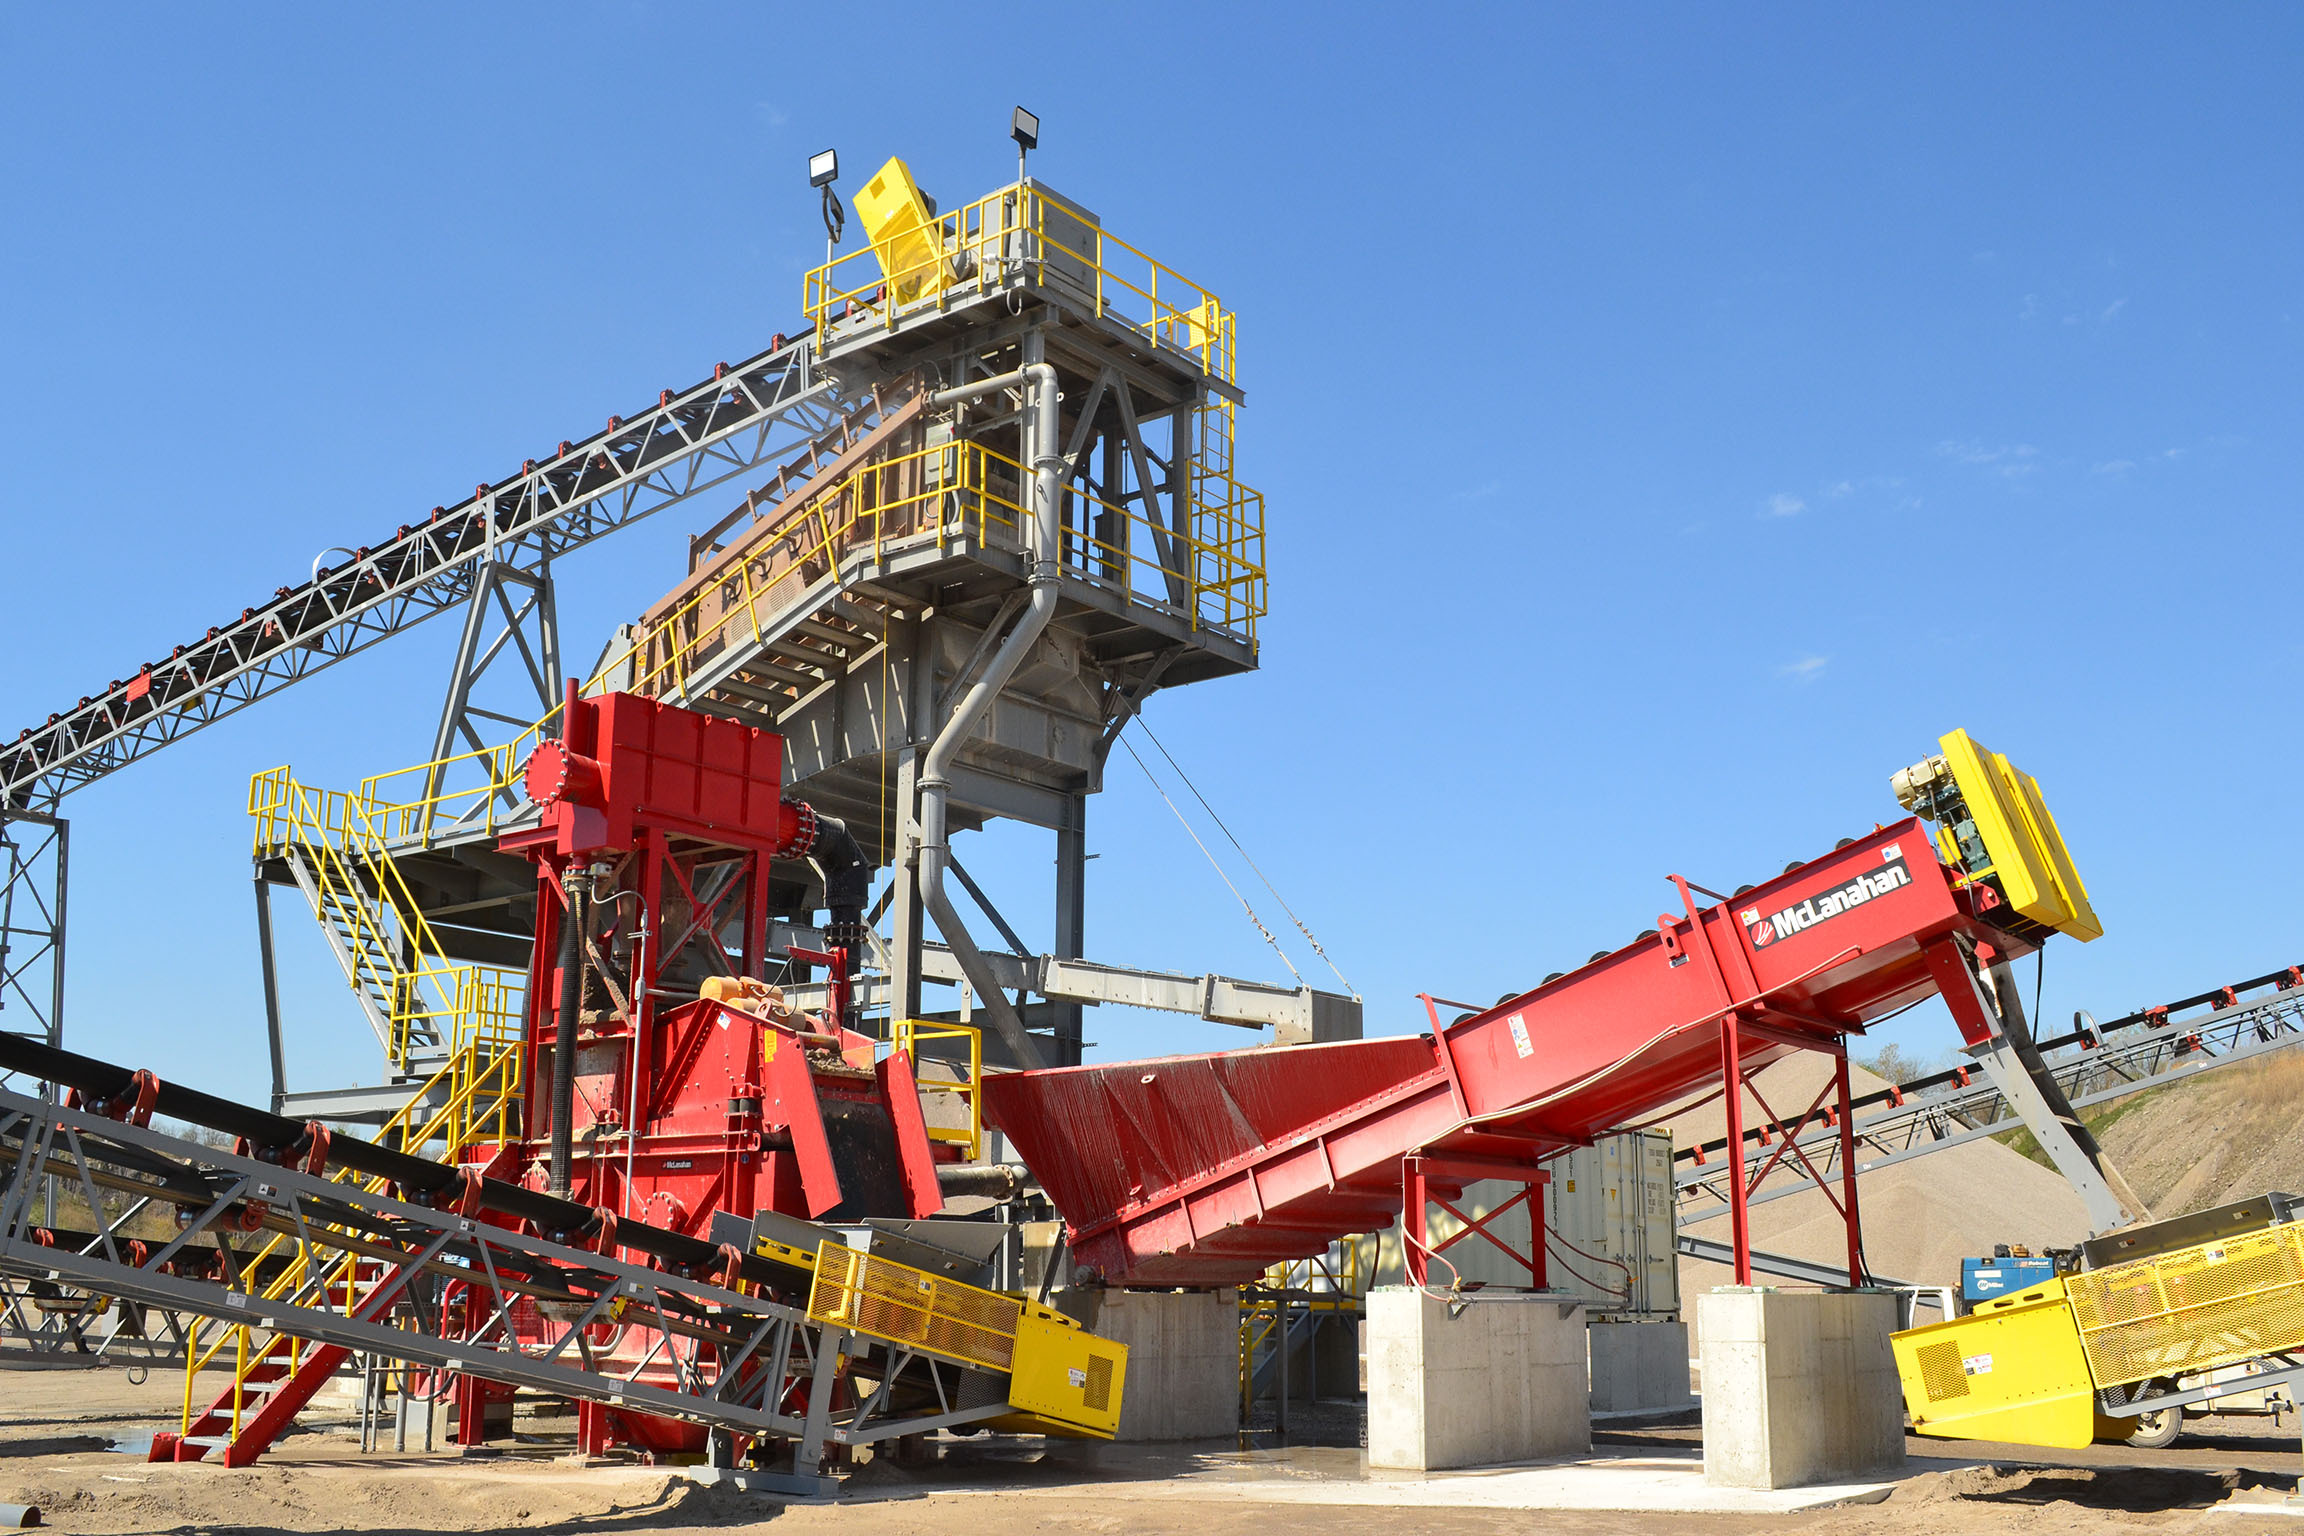
Working closely with their local dealer, Process Machinery Inc. (PMI), Custar Stone selected a McLanahan 44" x 33' Double Fine Material Screw Washer for the new plant. To further enhance efficiency and material recovery, they also incorporated an UltraFINES Recovery System (UFR) into the design.
This strategic equipment selection delivered multiple advantages. One of the most important benefits was the ability to avoid relocating the original screw washer during construction. Instead of disrupting operations, Custar Stone kept the original equipment running while installing the new system. Once complete, the original screw washer was repurposed at another operating site, maximizing the value of existing assets.
The new plant was designed with a streamlined and efficient process flow. Material is first sized into products such as 57s, 411s and 304 base material. Material passing through dry screening is then directed to an 8' x 20' triple-deck wet screen, where the operation produces finished 57s along with smaller aggregates like 8s and 9s.
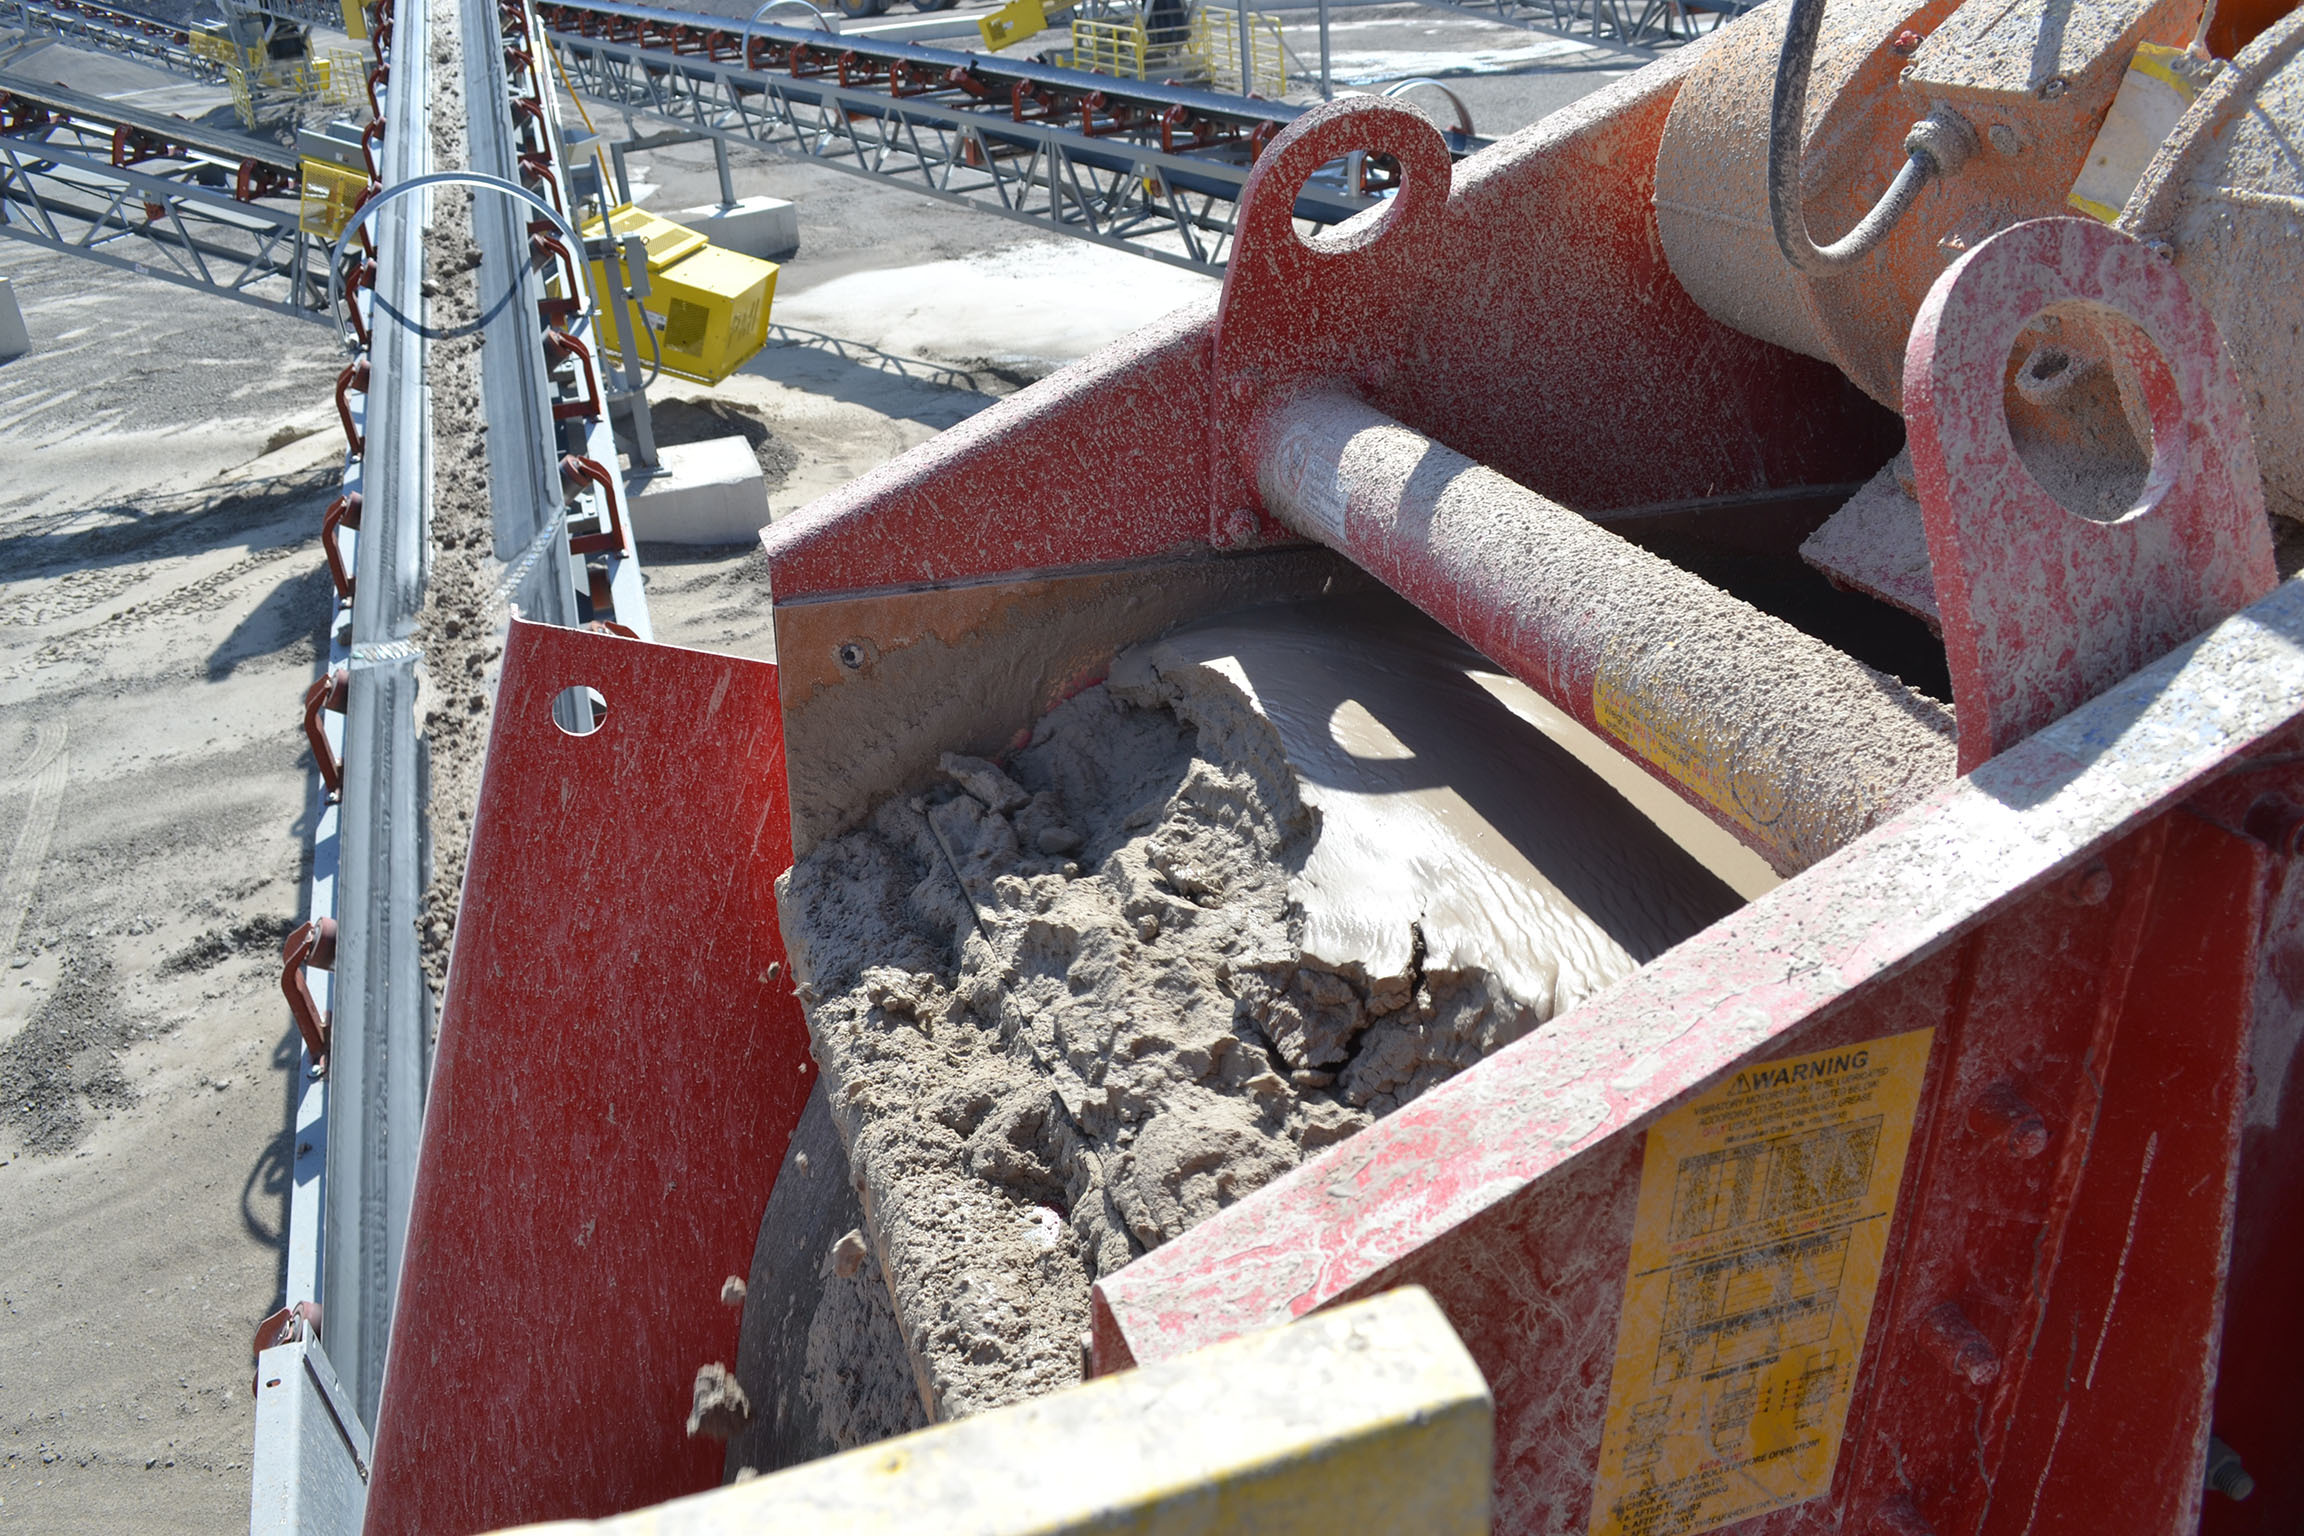
All undersized material from the wet screening process is fed into the McLanahan Double Fine Material Screw Washer, where it is cleaned and dewatered. Meanwhile, the overflow material is directed to the UltraFINES Recovery System. This integrated approach allows the plant to efficiently separate, process and recover valuable material that might otherwise be lost.
Results
The implementation of the McLanahan Double Fine Material Screw Washer and UltraFINES Recovery System delivered immediate and measurable improvements to Custar Stone’s operations.
The Double Fine Material Screw Washer is capable of processing up to 121 tons per hour, producing a clean, consistent and stackable final product. This level of performance supports higher throughput while maintaining product quality standards required for construction applications.
“McLanahan and PMI were here to help set it up, and once we got through that first little setup, it’s run without a hiccup,” Maassel said.
One of the most significant benefits came from the addition of the UltraFINES Recovery System. Traditionally, fine materials would be sent to a settling pond, requiring ongoing maintenance and periodic cleanout. This process not only consumed time and labor but also represented a loss of potentially valuable material.
With the UFR system in place, Custar Stone now captures these fine particles and converts them into a usable, marketable product. This innovation has significantly reduced reliance on the settling pond, minimizing maintenance requirements and improving overall operational efficiency.
“The biggest benefit of the McLanahan UFR is just not having to deal with that settling pond,” Maassel explained.
Beyond operational efficiency, the recovered material itself provides new revenue opportunities. The fine material is suitable for agricultural lime applications, where it helps neutralize soil acidity. It can also be blended back into certain aggregate products as a compaction aid, increasing its versatility and value.
“The UFR has definitely helped them with utilizing a product that was just going to be waste, dug out yearly, bi-yearly, out of the silt pond. Now, we got a sellable product that can go out on the trucks for multiple uses,” said Adam Coleman, Regional Sales Manager at Process Machinery Inc.