Introduction
Preventive maintenance is always cheaper than emergency repairs. The increased cost of overnighting parts and unplanned downtime can hit your operation in the pocketbook.
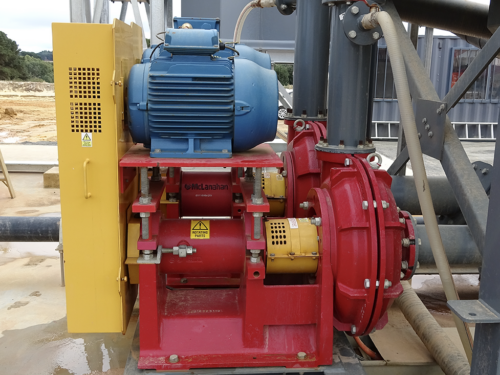
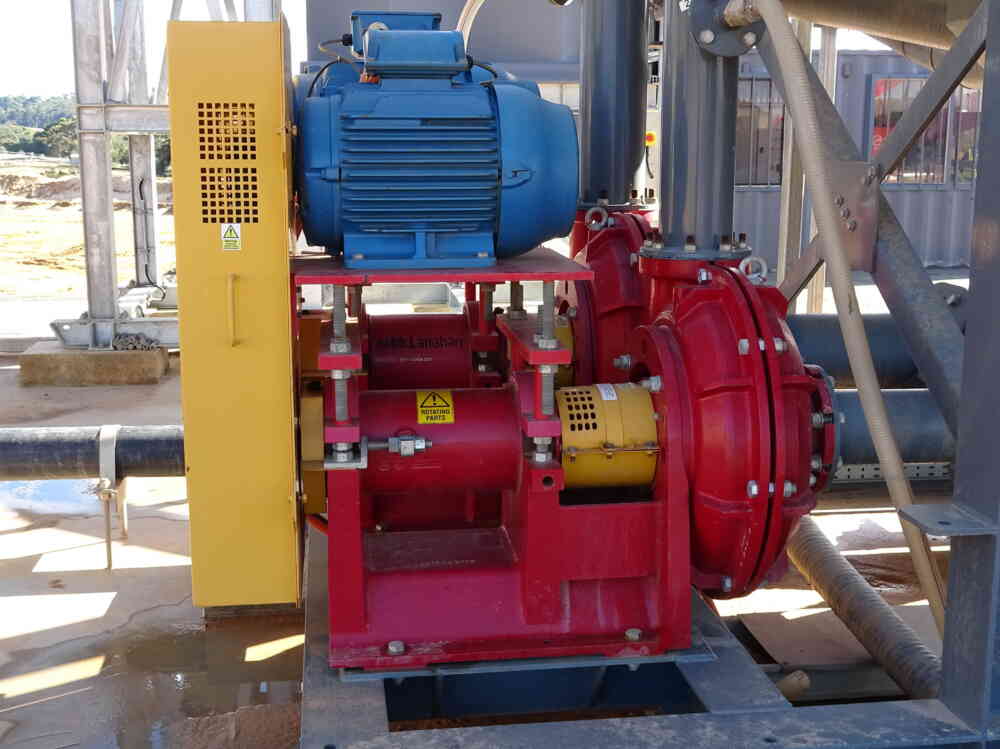
Although it is always good practice to open a pump for inspection, there are usually external signs of wear and tear because of the harsh environment in which pumps operate. By looking and listening for these signs, you can minimize surprise pump failures and treat the issue(s) with planned maintenance.
Note that automation can be used to alert you to some of these warning signs, while visual inspection is required for other warning signs.
Warning Sign No. 1 - Excessive gland leakage
Glands are used to keep fluid in the pump and prevent air from being drawn in. Some leaking from the gland is normal to cool and lubricate the sliding surfaces. There are different types of gland seals, and each has a different level of acceptable leaking. For example, a normal amount of leaking for a type D mechanical “dry” gland on a McLanahan Pump is between 5 and 55 drips per minute.
As an operator, you need to become familiar with what the gland leakage is supposed to be so that you can identify any issues. Excessive leakage can indicate a simple gland adjustment or maybe a small repair. Left alone, however, an excessively leaking gland will become a costly repair that could have been avoided. Operators should check the gland seal area for leakage at least once a day.
Warning Sign No. 2 - Excessive liner leakage
In the aggregate world, most slurry pumps have replaceable liners to protect the main body of the pump. Depending on how the liners have worn, the pump can leak out the liners. If ignored, the slurry will eventually wear the metal casing of the pump.
Product leakage is a clear sign that the liners may be worn or damaged. Excessive leakage should be addressed immediately by stopping production, opening the pump and inspecting the liners for damage. In the end, it is a lot cheaper and safer to replace the liners than it is to replace the casing and the liners.
Warning Sign No. 3 - Increased power consumption
Pumps require significant energy to move material through a pipeline, and over time that adds up. When power consumption increases, it is an indication that the pump is working harder to do the same job — or even worse, working harder and delivering less. The added energy cost does not help, but the loss in production can be extremely harmful to the bottom line.
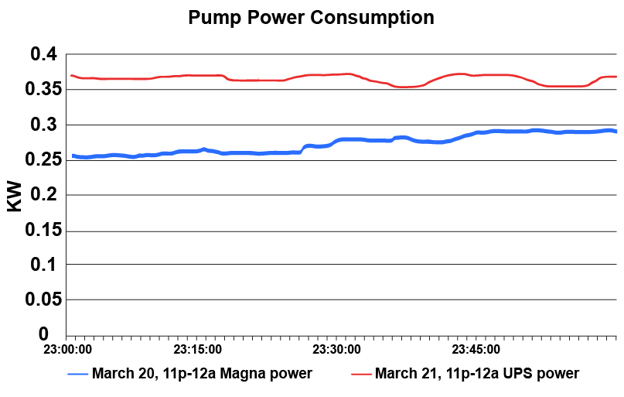
A sudden change in power consumption, whether it is an increase or a decrease, should always be a warning sign that something is wrong. Sudden increases in power demand can indicate air entrainment or damage inside the pump (such as worn liners or impeller), or it could be a result of plant changes around the pump.
Monitoring a pump’s power usage and setting warning parameters are an important part of keeping a pump in good working order. The best way to monitor a pump’s power usage is to have an automatic trending system, but even just manually recording data points is a good start. A structured monitoring program will put eyes on the equipment and can provide an early warning that something is wrong before it becomes a big problem.
Warning Sign No. 4 - Vibration
If a piece of equipment does not have vibration, it generally means it is not operating. Some equipment (such as screens) has a high level of vibration, while others feel more like a hum. With a pump, high levels of vibration can be a sign of inefficiency or worn elements. Worn bearings, turbulent flow and inadequate foundations are only a few sources of pump vibration.
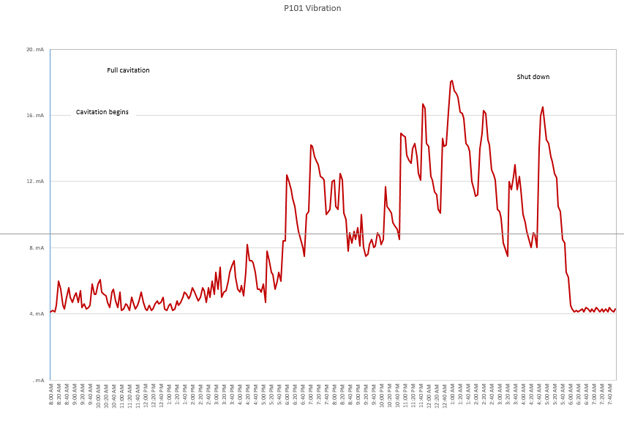
Pumps can be equipped with vibration monitors, which will track the progression of changes or spikes. Much like watching the power consumption, vibration levels will tell a story about the condition of the pump. Even without automated monitors, a good operator paying attention and doing daily walkaround inspections will know when something changes.
Warning Sign No. 5 - Bearing condition
The bearing assembly is an important part of any rotating equipment. Worn or damaged bearings can:
- Scar the shaft
- Cause vibration
- Create high noise levels
- Generate heat
- Decrease pumping efficiency
Because of the noise and vibration, you should be able to easily spot a worn or damaged bearing. Sites with extended times between visual inspections should install a vibration monitor to alert the team to any changes or spikes. A thermocouple or heat gun can be used to monitor the temperature level of the bearings and pump as well.
As any corrosion will rapidly accelerate the rate of wear, it is important to ensure the bearings are always well lubricated and not exposed to moisture.
Warning Sign No. 6 - Noise
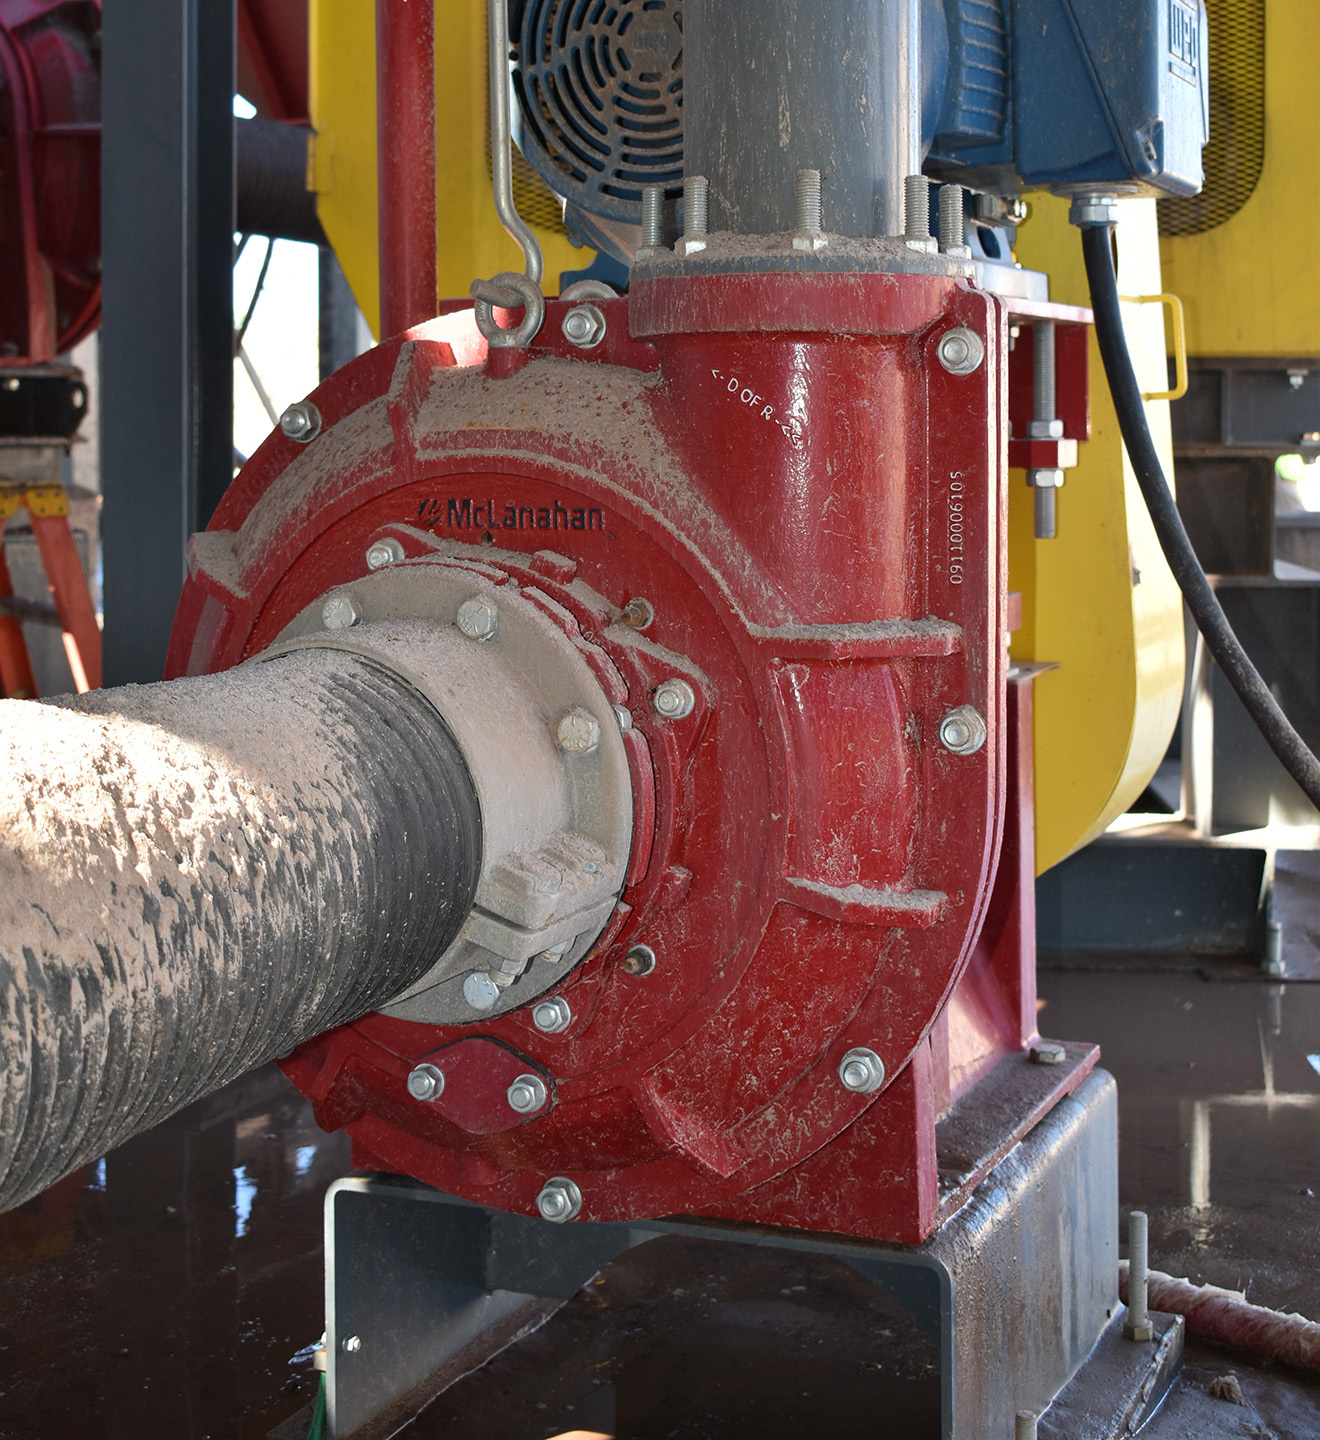
Listening to a pump can provide various early warnings. One of these warnings alerts you to a different type of wear caused by cavitation. Cavitation is simply the formation of bubbles or cavities in liquid, developed in areas of relatively low pressure around an impeller. Shockwaves form when these bubbles implode or collapse inside the pump, causing significant damage to the impeller, lining and/or pump housing.
Cavitation can cause:
- Failure of the pump housing, bearings and gland
- Destruction of the impeller
- Excessive vibration, leading to premature seal and bearing failure
- Higher than necessary power consumption
- Decreased flow and/or pressure
Listen at the suction and discharge end of the pump; cavitation generally sounds like marbles are going through the pump. Cavitation often happens suddenly and may also be observed by a sudden power reduction or dramatic drop in delivery pressure.
Operators should listen for unusual noise as part of their daily pump inspections.
Warning Sign No. 7 - Poor belt tension and alignment
The loud, squealing noise of loose belts is annoying, but the real harm comes from the heat generated that eventually causes the belts to fail. The slippage of a loose belt also causes a loss of energy transfer between the motor and the pump.
On the other hand, excessive tension or poor alignment will put a burden on the bearing assembly and the motor mount. In this scenario, something’s got to give, and it is usually the bearing assembly in the form of increased wear.
Excessive tension can also decrease pumping efficiency.
Warning Sign No. 8 - Wearing parts
Certain parts are designed to wear out to act as sacrificial components to protect others. In an operation, the slurry and operating points have a direct effect on the pump’s wear rate. As mentioned above, tracking energy consumption can indicate when the liners are wearing out, but nothing compares to physically examining them during downtimes.
This is why it is important to establish and follow a preventative maintenance schedule. Making time to regularly inspect wear components can give operators an idea of the life of those components and plan scheduled downtime for changeouts. When a process is stable, the liner wear rate should be predictable once a baseline is established. In this case, the passage of time can be a good sign of wear and indicate when it is time to change the liners.
Warning Sign No. 9 - Uneven wear on liners
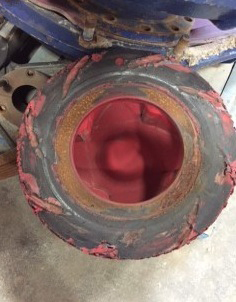
Liners will develop a pattern of wear under stable conditions. Unexpected wear points can direct you to signs of trouble, such as:
- A highly turbulent flow passage
- Misapplication or sizing of equipment
- Incorrect operating points
- Unsuitable materials of construction
Again, creating and sticking to a regular inspection schedule that includes occasionally opening the pump up for inspection will allow you to identify any unusual wear patterns.
Warning Sign No. 10 - Poor pump performance/flow rate
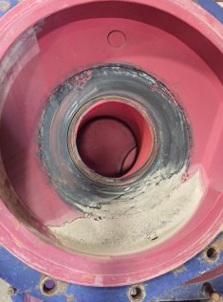
Monitoring a pump’s flow rate has multiple advantages in relation to how well a process is performing, but it can also give insight into wear components within the pump. A reduction in flow rate can be caused by several issues (such as an obstruction), but a consistent and long-term decrease in the flow rate will generally be a reflection of worn liners and impellers.
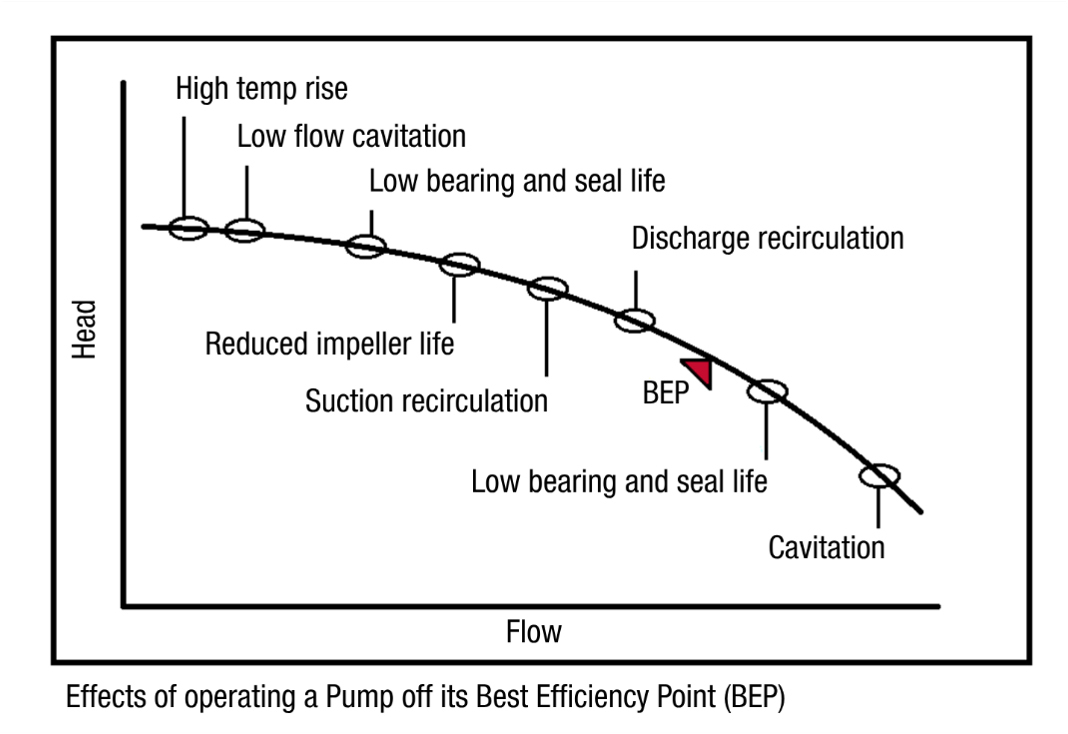
Every pump has a Best Efficiency Point (BEP) on its operation curve. Knowing where your pump is operating on the curve in comparison to the BEP can give you a heads-up to potential problems. When a pump slips in its performance, as shown by the flow rate, it moves away from its BEP and increases wear and tear on the pump.
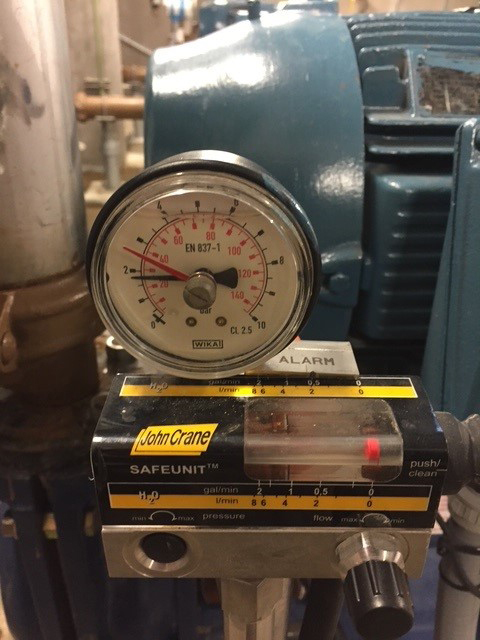
Dependable flow meters can be a significant investment, but they can provide valuable insight for the process and pump’s condition.
Warning Sign No. 11 - Repeated failures
A pump will break down sooner or later — that is a given. When the same pump has repeated failures over a short period of time, it is an indication that something is substantially wrong. Whether it is the wrong pump for the duty required, poor quality replacement parts or an improper repair procedure, repeated failures are a sign the overall pump installation needs to be reviewed.
Tracking and documenting repairs can help pinpoint the issue and allow a long-term fix to follow. In many cases, a repurposed pump can be undersized or oversized for the application. Both of these situations can cause problems as shown by the “Effects of operating a pump off its BEP” chart above.
It is a costly and frustrating lesson to learn, but when a pump fails multiple times in a short period of time, it is a good time to bring in the manufacturer for a review.
Warning Sign No. 12 - Line pressure
Without a flow meter, the flow rate can be monitored indirectly via another method. A constant flow rate in a constant pipeline volume will produce a constant line pressure. A change in line pressure may not tell you exactly what has changed, but it will tell you something has changed. When it comes to pumping slurry, unexpected changes are bad news.
Warning Sign No. 13 - Air in discharge
Anyone who has been around pumps knows that air and centrifugal pumps are not friends. Air in the pump can lead to several issues, either with the pump itself or downstream equipment. It can lead to cavitation, which, as mentioned above, will cause damage to the pump surfaces. A pump can also become airlocked when the air forms pockets, which disrupt the flow of slurry. This is most common on pumps with bottom horizontal discharge.
Equipment downstream, such as Hydrocyclones and Separators™, will be negatively affected if there is entrapped air within the slurry. Air in the slurry disrupts the air core inside the cyclone and can lead to bypass in the overflow. With Separators™, air in the slurry will prevent a siphon from forming, which is necessary for proper operation. Slurry will either pour out of the bottom of the Separator™ or, less likely, short circuit into the overflow.
Air in the discharge can be prevented by making sure the sump is not vortexing, the slurry level is not too low, and the slurry is not plunging in and entraining air. If the pump is cavitating, the entire pumping system should be reviewed to ensure the Net Positive Suction Head available (NPSHa) — before the pump — exceeds the Net Positive Suction Head required (NPSHr) — after the pump.
Warning Sign No. 14 - Sump level
Dramatic swings in the sump level can indicate a number of issues with the pump itself, but it can also cause problems to the pump. Since a centrifugal pump requires a head to operate, changes in the head (as shown by the sump level) can point to future and current problems.
For example, if the sump capacity is inadequate, the pump can fail to discharge on startup. Minimum sump capacity should equate to at least one minute’s pumping time in many instances. If the sump level is too low, the pump will draw in air with the slurry and cause additional problems.
Warning Sign No. 15 - Poor downstream equipment performance
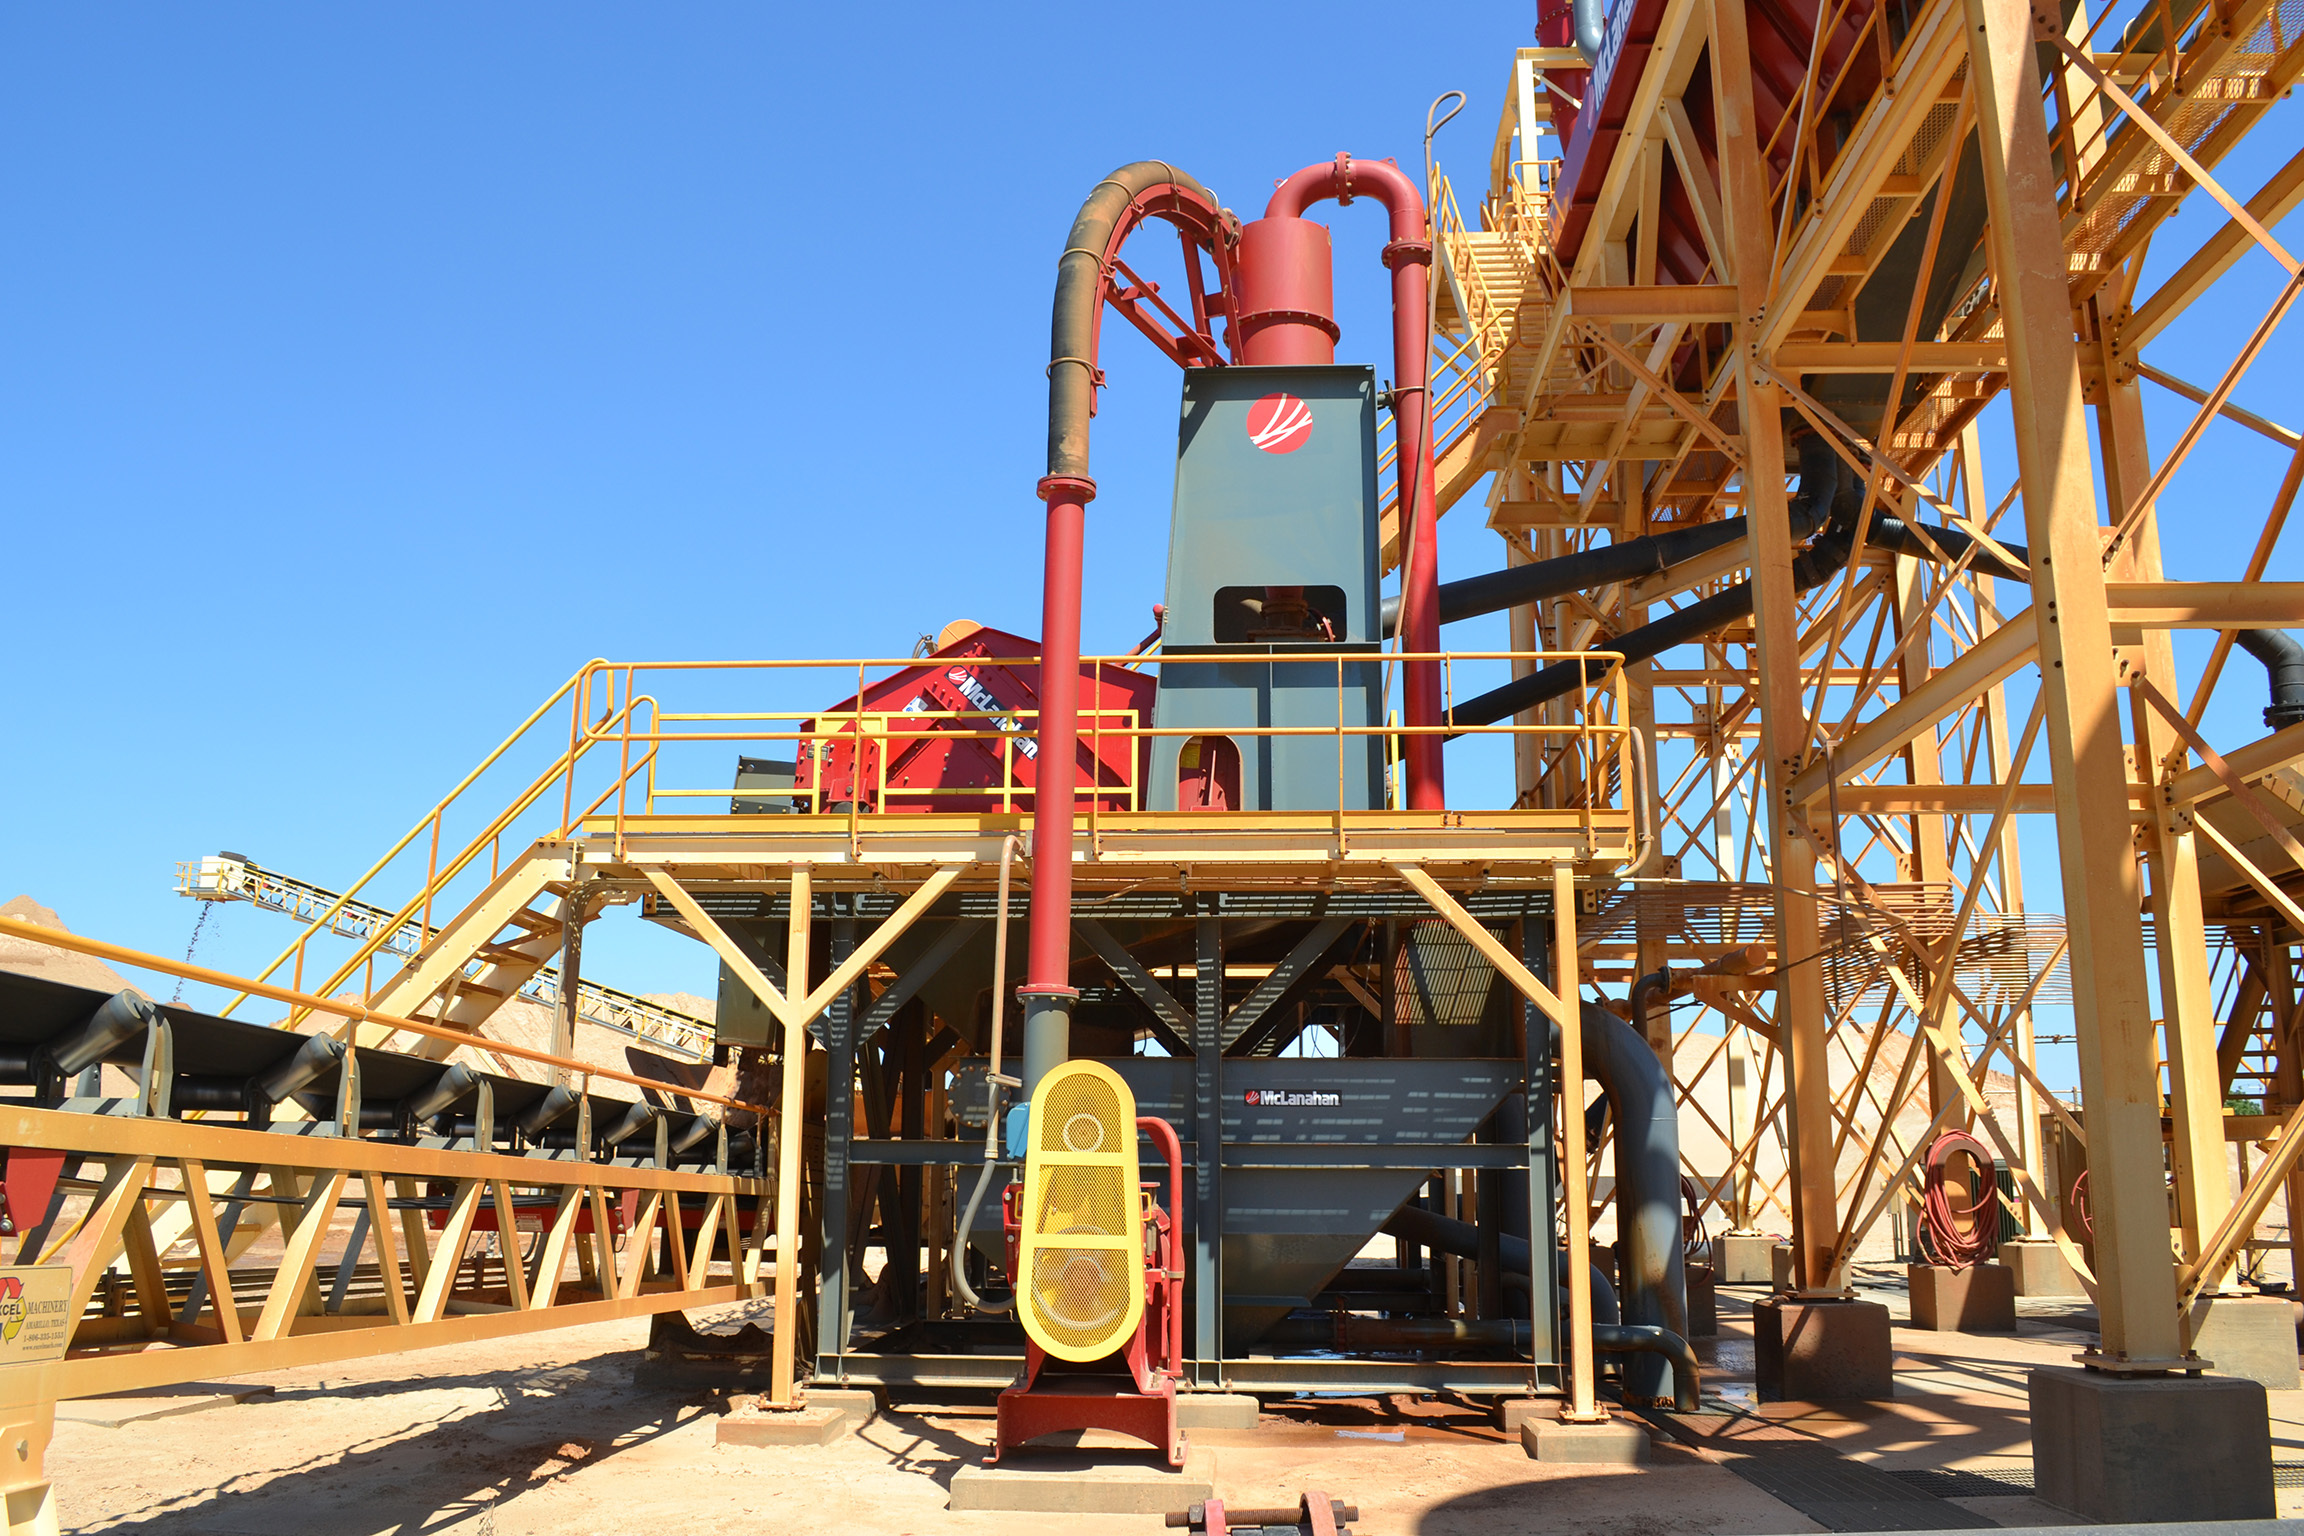
While a pump is only providing material handling, the downstream equipment usually requires that the slurry falls within specific parameters. In the case of a Hydrocyclone, changes in the flow rate (as provided by the pump) will change the cut point of the cyclone – you may notice the discharge is coarser or finer than desired. Air in the line from the pump will disrupt a Separator™’s ability to form a siphon, which is essential for producing a drier underflow, so this may cause the Separator™ to flush. These are just some examples of how poor downstream equipment performance can indicate pump problems.
When downstream equipment is not functioning properly, the overall performance of the process can be severely harmed. A pump is an important part of any wet process system, and when the pump is not performing, the signs show up everywhere downstream.
The pump will tell you when it is in trouble. You can listen for the whisper and have plenty of time to address the issue, or you will hear it scream in the middle of the night.